- Publisher:admin
- Time:2026-10-10
- Clicks:3
- Source:
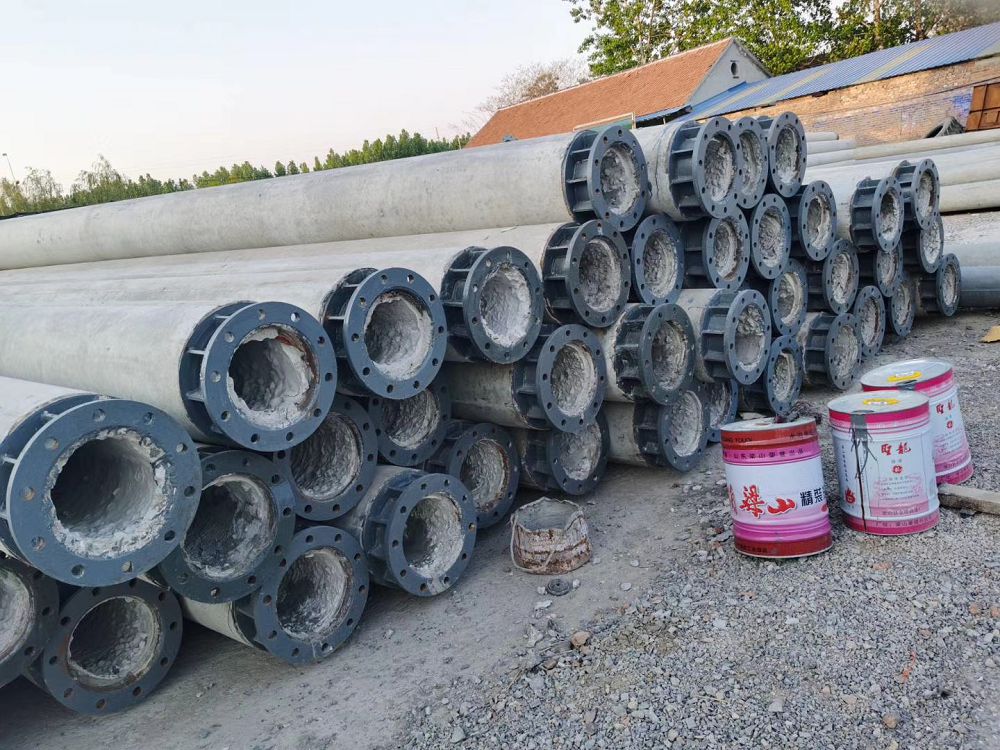
A qualified concrete utility pole passes through many production stages before it leaves the factory. Centrifugal casting, prestressing, and steam curing are well-known terms, but behind them is a practical manufacturing system built on process control and experience. This article walks through the key steps of concrete pole production.
1. Steel Cage Fabrication: Forming the Skeleton
The first major step is fabricating the steel cage. Longitudinal prestressing tendons are arranged around spacer rings according to design requirements. Non-prestressing bars are welded or tied at intersections. Spiral reinforcement is wound continuously around the longitudinal tendons to form a three-dimensional cage.
Modern production lines often use digital seam welding machines. Computer-controlled resistance welding wraps the spiral wire precisely around the longitudinal bars. End rings are welded at both ends. The cage geometry and weld strength are checked to ensure they meet design requirements.
The accuracy of the steel cage directly affects the mechanical performance of the finished pole. If longitudinal tendons shift, bending stress distribution may become uneven and load capacity may be reduced. If spiral spacing is too large, confinement and crack control may be weakened. Therefore, dimensional inspection is an essential quality step in cage fabrication.
2. Mould Assembly and Prestressing: Preloading the Structure
After fabrication, the steel cage is placed into a steel mould. For prestressed poles, prestressing is applied before centrifugal casting. Tensioning forces commonly range from about 1,000 kN to 1,900 kN, depending on design. The tendons are stretched to a designed stress level before concrete is placed.
The principle is straightforward. The steel is stretched before the concrete hardens. After the concrete gains sufficient strength and bonds to the steel, the tensioning force is released. The elastic recovery of the steel compresses the concrete. This pre-compression helps the pole resist cracking under service loads.
For outdoor poles, fewer cracks mean less water and aggressive ion ingress. This reduces the risk of reinforcement corrosion. This is one reason prestressed poles can perform well in corrosive environments.
3. Concrete Placement and Centrifugal Casting: Creating a Dense Core
Concrete placement gives the pole its “body.” Cement, sand, stone, water, and admixtures are weighed according to the mix design and mixed thoroughly. The concrete is then distributed into the steel mould.
Centrifugal casting is a distinctive core process for annular concrete poles. It is usually carried out in stages. In a typical sequence:
-
Low-speed centrifugation at about 100 rpm for 2 minutes to distribute concrete evenly.
-
Medium-speed centrifugation at about 300 rpm for 2.5 minutes to densify the concrete.
-
High-speed centrifugation at about 400 rpm for 9 minutes to expel excess water and achieve dense packing.
During high-speed rotation, centrifugal force can reach many times the force of gravity. The effective water-cement ratio can drop from above 0.6 in the mixed concrete to around 0.3. This reduction significantly increases strength. Centrifugally cast concrete can be 20% to 30% stronger than ordinary vibrated concrete with the same mix proportions.
The centrifugal process also forms a uniform tubular structure. The inner surface is smooth, which helps later cable installation. After centrifugation, residual slurry inside the pole should be removed. If left in place, it can form a thick layer, increase weight, and create shrinkage stresses.
4. Steam Curing: Accelerating Strength Development
After centrifugal casting, the pole remains in the mould and enters steam curing. The curing process usually includes four stages: static pre-curing, temperature rise, constant temperature, and temperature drop.
-
Static pre-curing allows the concrete to set slightly before heating. This helps prevent surface cracking.
-
Temperature rise increases the temperature at a controlled rate.
-
Constant temperature keeps the temperature stable so cement hydration can proceed.
-
Temperature drop lowers the temperature slowly to avoid thermal stress.
A typical steam curing regime may involve curing at about 80°C for 7 hours. The concrete strength grade should reach at least C50 before demoulding, and the strength at demoulding should not be lower than 70% of the design strength. For higher-strength concrete poles, prestressing tendons should be released only after the concrete reaches the specified strength, such as C60 or above.
The purpose of steam curing is to accelerate hydration. Natural curing may require 28 days to reach design strength. Steam curing can shorten this period to several days or even hours. However, temperature and time must be controlled carefully. Excessive temperature or time can create microcracks and reduce durability. Insufficient temperature or time can leave the concrete below the required strength.
5. Demoulding, Inspection, and Delivery
After steam curing, the pole is demoulded. It then passes through appearance inspection, dimensional measurement, and mechanical testing.
Appearance inspection checks for honeycomb, pitting, exposed reinforcement, and other defects. Dimensional checks include:
-
Pole length tolerance: ±10 mm
-
Wall thickness tolerance: ±3 mm
-
Top diameter tolerance: ±2 mm
-
Ovality: ≤5 mm
-
Bending deviation: ≤1/1000 of pole length
Mechanical testing is a key part of factory inspection. A bending test is often performed on a horizontal test bed. One end of the pole is fixed, and a hydraulic jack applies load in stages at the other end. The cracking load, ultimate capacity, and deflection are recorded.
According to standard requirements, under the load-carrying capacity test moment, the crack width in the tension zone should not exceed 0.20 mm. There should be no crushing of concrete in the compression zone, no rupture of reinforcement, and no overall instability. Only poles that pass all required tests receive a factory certificate and are released for delivery.
Every qualified pole is the result of raw material quality, process precision, and quality control working together.